Why 90% of Top Mines Switched to Peristaltic Pumps for Flotation Reagent Dosing?
In the flotation process of minerals such as copper, gold, and lithium, the precise addition of chemical agents such as collectors, frothers, and inhibitors directly determines the grade and recovery rate of the concentrate. However, the characteristics of strong corrosiveness (such as cyanide), high viscosity (flocculant), and solid containing agents (lime slurry) make diaphragm pumps and centrifugal pumps face fatal problems:
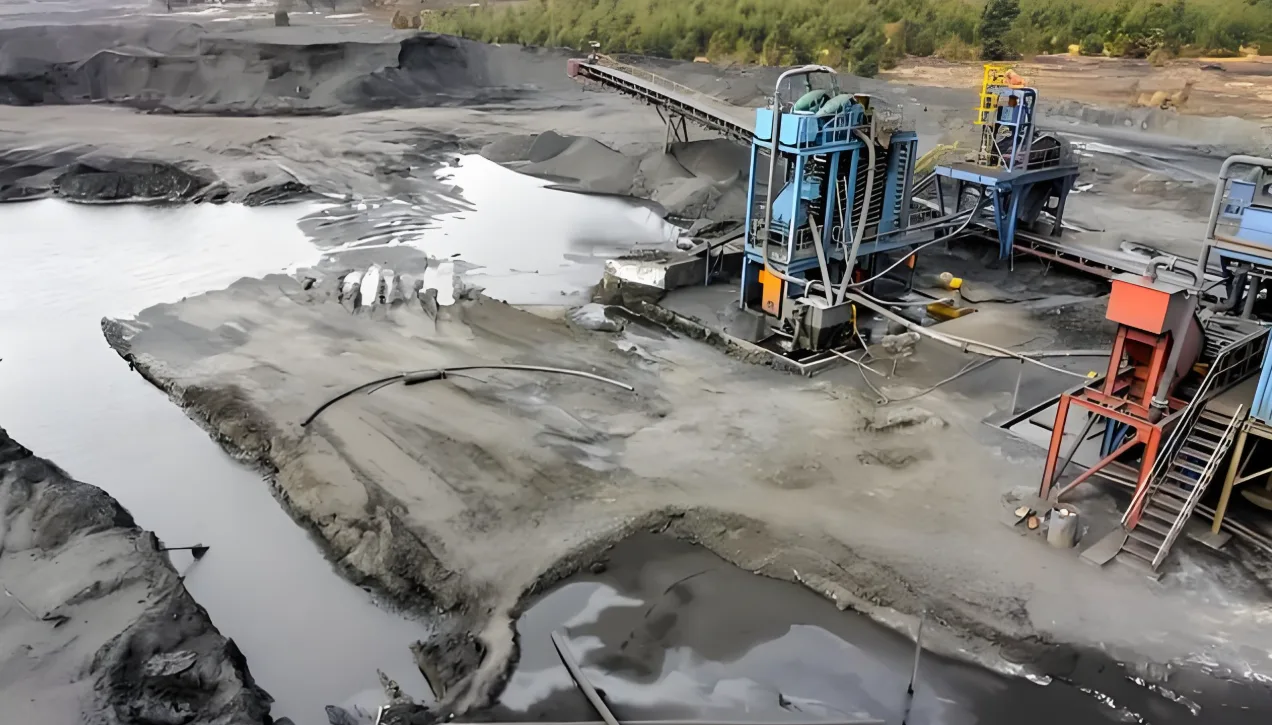
1. Sealing failure and leakage: Hazardous chemicals threaten personnel safety
2. Maintenance costs skyrocket: Mechanical seal/valve replacement accounts for 60% of pump lifecycle costs
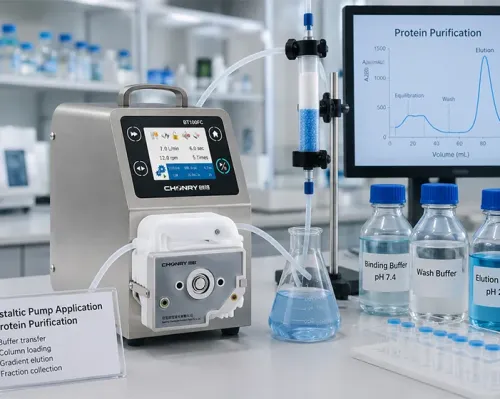
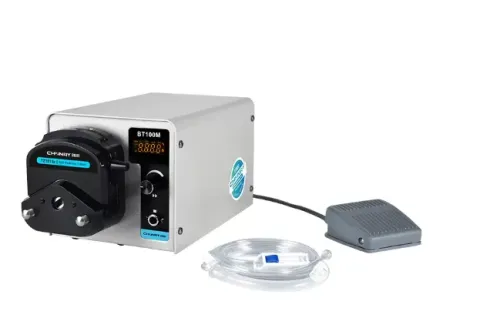
The peristaltic pump uses rotating rollers to squeeze elastic hoses, generating vacuum suction and conveying power to transport liquids. During the transmission process, the fluid is 100% sealed inside the hose, completely eliminating the risk of leakage.
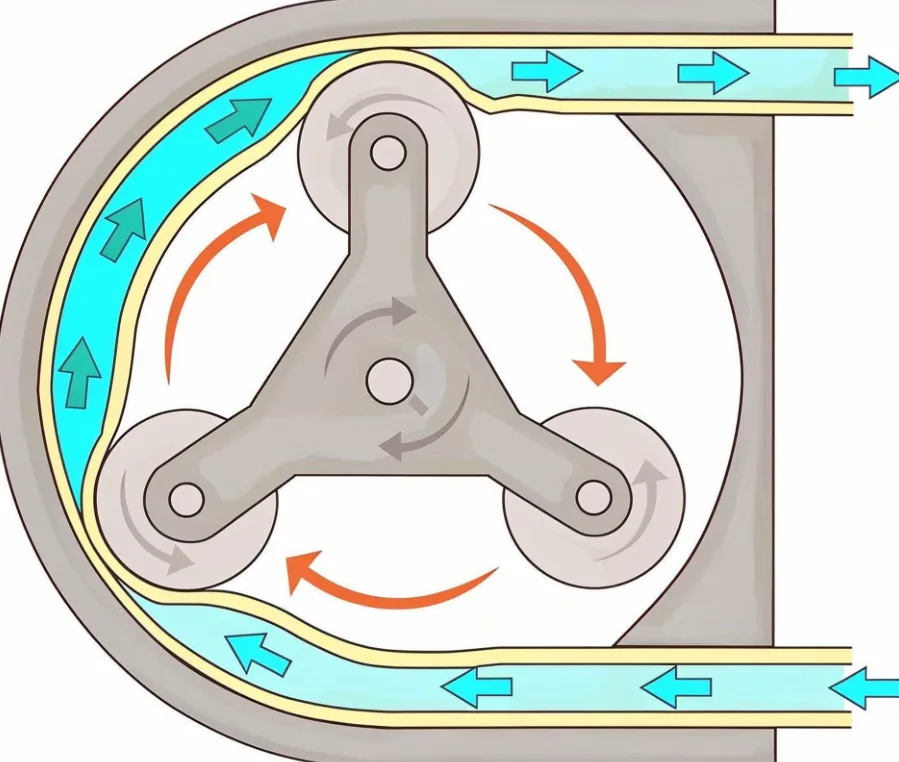
Case: Norprene used in a Chilean copper mine ® By using a hose pump to deliver 30% concentrated hydrochloric acid and replacing the leaking diaphragm pump, the annual reduction in chemical losses is $180000 uch as Viton) ® Fluorine rubber resistant to cyanide corrosion
Four key application scenarios for flotation plants
1. Collection agent injection: precise control of trace amounts of yellow medicine/black medicine (flow range 0.1-2000mL/min)
2. Foaming agent addition: foam stability control of methyl isobutyl methanol (MIBC)
3. Inhibitors delivery: Safe zero leakage treatment of sodium cyanide
4. Online analyzer sample supply: High consistency slurry supply for XRF analyzer
Successful transformation of Peruvian silver mines
Problem: The diaphragm pump frequently leaks arsenic inhibitors, with an annual maintenance cost of $86000
Solution:
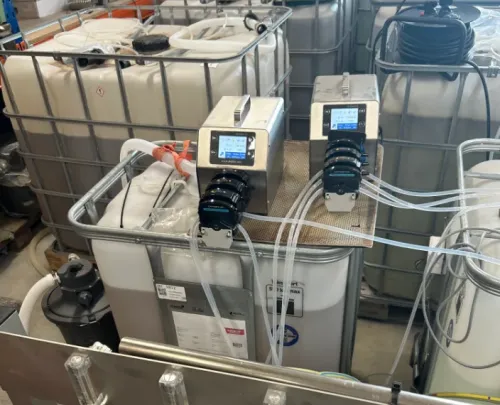
Deploy 3 Chonry BT300 LC series peristaltic pumps (Viton) ® Flexible hose)
Integrated PLC proportional control system
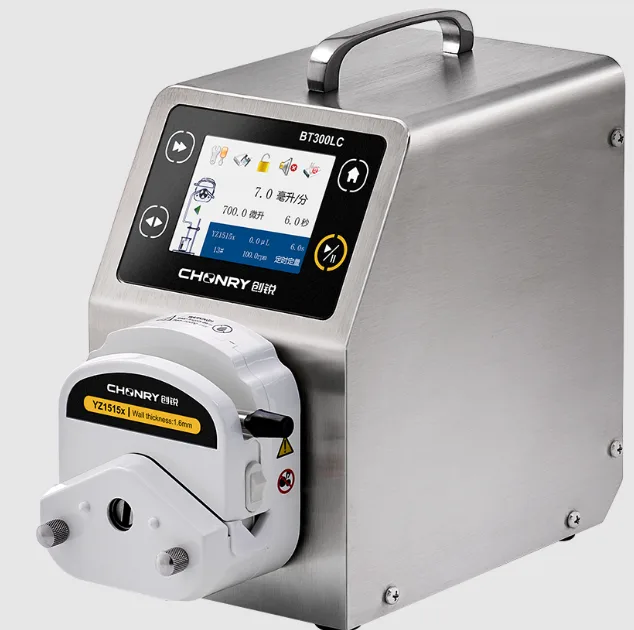
result:
Reduce medication consumption by 18%
54% reduction in maintenance costs
Silver recovery rate increased by 2.3%
The zero leakage design of the peristaltic pump allowed us to pass our EPA compliance audit in one go! ”On site engineer Luis M