Industry Applications
Bơm nhu động trong y tế, dược phẩm, thực phẩm – đồ uống, xử lý nước, in ấn – bao bì và công nghiệp nặng.
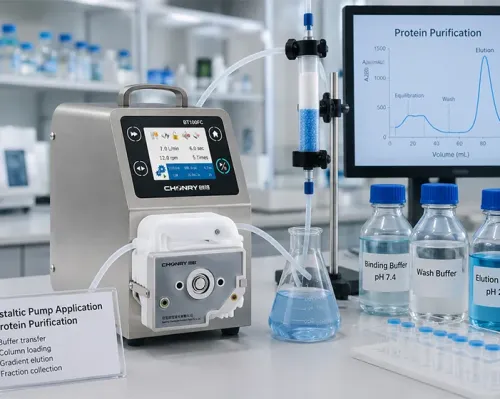
Peristaltic pumps are indispensable in protein purification, offering low-shear fluid handling, easy sterilization, and excellent chemical compatibility.
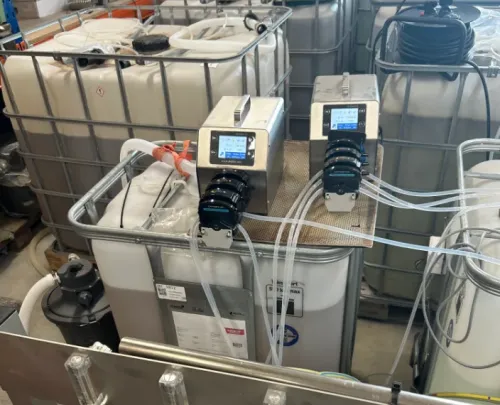
Whether it's industrial filtration, water treatment filtration, laboratory filtration, or pharmaceutical filtration, choosing the right peristaltic pump can effectively improve filtration efficiency, extend the life of the filter membrane, and reduce production costs.
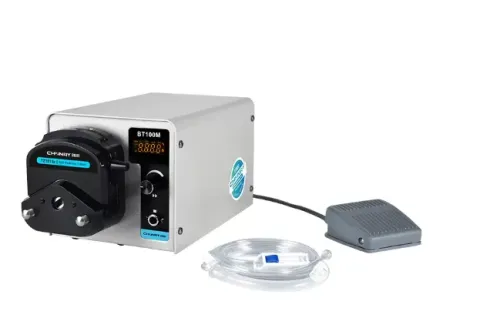
Professional choledochoscope peristaltic pump solution, providing stable perfusion, low pulsation delivery and precise flow control. It is widely used in electronic choledochoscopes, disposable choledochoscopes and endoscope systems, and supports CE/FDA standards and OEM customization services.
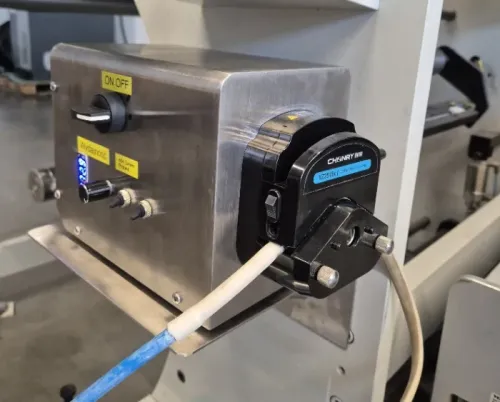
Chonry Peristaltic Pump has 16 years of experience in the peristaltic pump industry. We have customized a peristaltic pump to match a single-brush machine according to the customer's requirements. This solution has been highly recognized by the customer. If you have any needs for customized perist
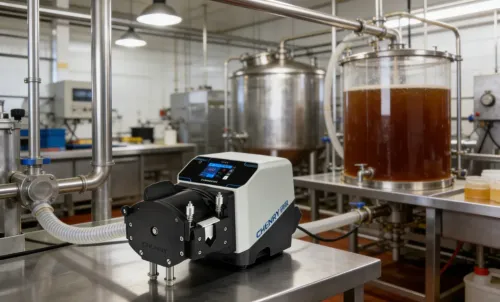
A peristaltic pump works well with viscous liquids such as syrup because the fluid moves through a flexible tube that is compressed by rollers. This design maintains stable flow and prevents clogging, which often occurs with other pump types when handling thick liquids.
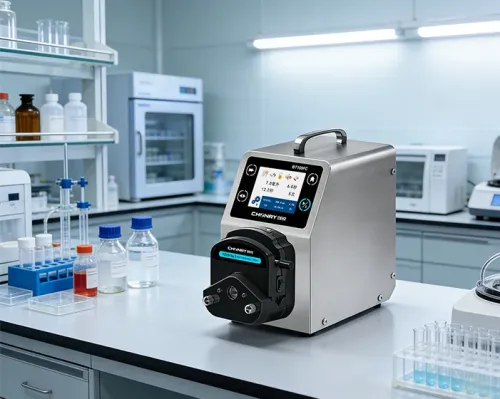
Learn how a peristaltic pump used in pharmaceutical industry ensures sterile fluid transfer, precise dosing, and safe production. Explore types and applications.
Applications of peristaltic pumps in the laboratory
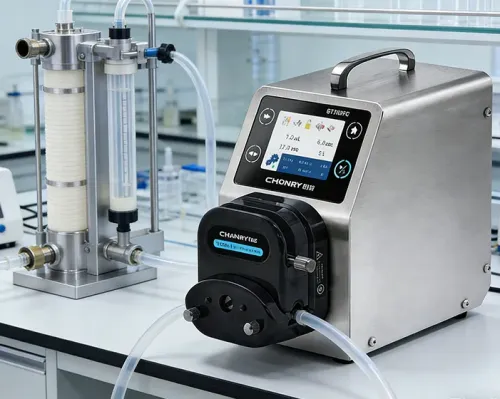
The working principle of a peristaltic pump is simple and effective: rotating rollers or sliders sequentially compress a flexible tube, creating a moving blockage that propels the fluid within. This design ensures that the liquid only contacts the inner wall of the tube, not the pump body itself. Th
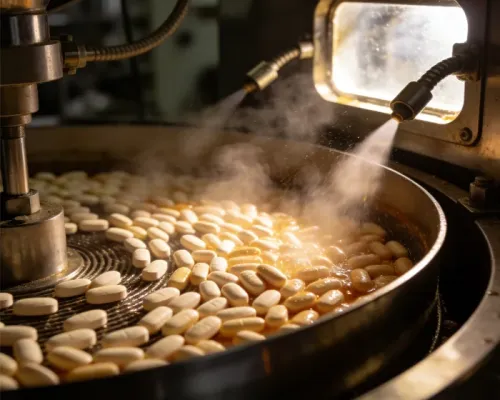
The pharmaceutical and nutraceutical industries face relentless pressure to enhance product quality, ensure batch-to-batch consistency, and improve manufacturing efficiency. Film coating, a critical unit operation for tablets, pellets, and granules, sits at the heart of this challenge.